


Above: Carbide-tipped blades can handle difficult-to-machine steels, high-alloy metals, titanium, stainless steel, Inconel and more.
September, 2026- Horizontal band saws are still the machine of choice for service centers— from manualfeed up to fully automated CNC lines. And “bi-metal blades are still what most reach for first,” says Felipe Arntsen, product manager, saws & HPTA, for the L.S. Starrett Co., Athol, Massachusetts. They’re “reliable and cost-effective for the carbon steel that makes up most of what gets cut.”
As service centers branch out into a broader mix of materials, including harder alloys, bimetal “doesn’t always cut cleanly or last long,” Arntsen says. “That’s pushed more customers toward carbide-tipped blades, which hold up better under those conditions. That’s part of why Starrett has invested into developing blades like the Advanz line, which is built for that harder, more abrasive end of the range.”
UNDER PRESSURE
The Advanz line’s carbide tips are ideal for cutting extremely hard, abrasive materials because they withstand extreme cutting pressure and offer a high resistance to wear and fatigue. For materials such as high-alloy metals, titanium, stainless steel and Inconel, a carbide-tipped blade with a multi-chip grind offers faster cutting to maximize productivity and blade life.
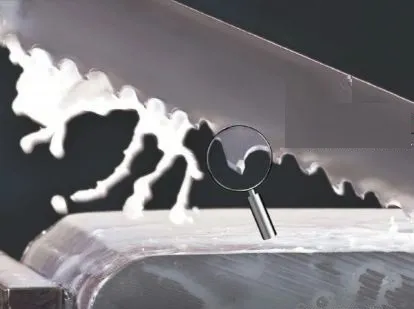
Advanz TS features teeth ground from micro-grained carbide cylinders welded to a tough, ductile backing material.
“The blade has a direct effect on cost per cut,” says Arntsen, “and that’s what service centers actually care about—not just the price of the blade itself. A blade that holds its edge longer means fewer changeovers, which keeps the machine cutting instead of sitting idle for setup and blade swaps. Fewer changeovers also means less blade inventory to manage, which matters for service centers trying to control tool costs across a wide mix of jobs.”
He points out that blade life also is tied to “matching” the tool to the job. “Cutting the material with the wrong blade will wear out the blade faster, so a cost-effective choice isn’t always a lower-cost blade or an incorrectly specified blade. It’s the blade that fits the application best and doesn’t need replacing halfway through a run that ultimately provides the best cost per cut.”
The right blades also cut cleanly, reducing scrap and rework, “which has its own cost even before you factor in blade or machine time,” Arntsen points out.
RECIPE FOR SUCCESS
When selecting a blade, it’s important to know what materials you’re cutting, says Arntsen. “Carbon steel is the still the bread and butter for most service centers, but many sawing operations today are running a broader mix and there’s no one-size-fits-all blade for that.
“Most service centers also don’t want to be swapping blades every time the job changes since carbide costs more, and switching back and forth eats into productivity,” he continues.
Starrett’s Primalloy is a bi-metal blade built for heavy-duty cutting, alloyed with cobalt and vanadium “to get closer to carbide-level performance at a bi-metal price, so it covers more ground without forcing a switch,” Arntsen says. “It’s a good fit across a range of jobs, but once you hit the harder-to-machine metals, such as Inconel or Hastelloy, bi-metal just won’t cut it, and carbide-tipped is worth the extra cost.”
For structurals, pipes, tubes and bundles, the Starrett Tennax-Pro line is “built for the mixed-profile cutting that’s a daily reality in most service centers,” notes Arntsen. TennaxPro blades feature high-speed M-42 steel teeth and a special tooth geometry that dissipates stress during cutting, while also reducing vibration and noise.
Setting the machine up for success matters just as much as the blade including tension, tracking and guide condition, says Arntsen. “Even the right blade for the material won’t perform well on a saw that’s out of tune.”
Many service centers are also moving toward smart automation on their saws, giving them the ability to catch blade wear or a problem before it causes a bad cut, blade damage or downtime due to maintenance needs.
“This also plays into safety since the machine is watching for issues that an operator might not catch until it’s already a problem,” concludes Arntsen.
BLADE TIPS
LONGEST LIFE
Understanding the material characteristics helps achieve the longest band saw blade life and production efficiency. There are several visual clues that can indicate a loss of cut quality:
• Backer fractures or signs of wear on the back of the blade.
• Tooth wear. Once teeth are damaged, their clearances and angles will be different. Adjust speeds and feeds to avoid over penetration and tooth strippage. In general, use slower speeds for harder materials and faster speeds for softer materials.
• Wavy, rough and uneven cuts. As a saw blade degrades, the quality of the cut deteriorates.
• Scoring of the blade by the guides. This is usually a sign of insufficient coolant fl ow, which increases heat and friction, damaging the blade.
• Work hardening. If teeth are not properly penetrating the material, the blade will rub the material instead of cutting it, which causes premature dulling.
• Excessive noise. As the blade wears over time, the band saw can generate a loud whining or grinding sound. Noise can also occur more when using constant pitch blades, whereas variable pitch blades evacuate chips more efficiently in the cut, reducing harmonics.
The L.S. Starrett Co., http://starrett.com/